

Anyone who uses more than three or four tools per part on a CNC milling machine knows the problem: every manual tool change costs one to three minutes of machine downtime, plus there is the risk of incorrectly set tool lengths. An automatic tool changer (ATC) with SK30 holder solves both issues at the same time. SK30 has established itself as an industry standard in wood, plastic and aluminium machining because the holder is robust, delivers high repeatability and works in a speed range that suits the typical 5 to 20 kW milling spindle.
In this guide we explain how SK30 is constructed, which magazine types exist, how SK30 compares with HSK and ER, and which BZT series offer the tool changer as standard or as an option. If you want to retrofit an existing machine, you will also find an assessment at the end.
What is SK30? The tool holder explained
SK stands for steep taper (Steilkegel), and the number 30 stands for the taper size according to DIN 69871 or ISO 7388. The taper has a ratio of 7:24 and therefore a very shallow taper angle, which creates a non-self-locking connection: the spindle can release and eject the tool again without force. Clamping is done by a pull stud, which a disc spring system in the spindle tightens with typically 800–1200 daN.
Advantages of the SK30 holder:
- Repeatability: With good spindles, the radial repeatability is below 5 µm, which is decisive for dimensionally accurate parts.
- Speed range: Up to approx. 24,000 rpm, depending on the spindle manufacturer and balance grade.
- Standardisation: Holders, collets, shrink-fit chucks and cutters are available worldwide.
- Robustness: Stable even under lateral loads in aluminium or light steel use.
SK30 is therefore the sweet spot: large enough for serious machining, small enough for compact milling spindles with a power of 5–20 kW. If you are looking for the matching holder, you will find a wide selection in our CNC accessories, from ER collet chucks to shrink-fit chucks.
Manual vs. Automatic Tool Change
With a milling spindle with an ER collet, you change the tool manually: loosen the clamping nut with two wrenches, remove the old cutter, insert the new cutter, tighten the nut again, then touch off or measure the tool length. This works for simple parts, but quickly becomes a bottleneck.
Advantages of manual changing:
- Low purchase cost: a spindle with an ER collet is the lowest-cost option.
- The tool can be of any height or length, no magazine position needed.
- Entirely sufficient with 1–3 tools per part.
Advantages of automatic changing (ATC):
- Change time per tool: 3–8 seconds instead of 60–180 seconds.
- Unattended machining, which matters for long programs or night operation.
- Reproducible tool lengths through probe measurement after every change.
- Fewer operator errors (wrong cutter clamped, forgetting to tighten).
Rule of thumb: from four tools per part, or from series production with 20+ pieces, an ATC pays for itself very quickly. More on this in the ROI section below.
ATC Magazine Types at a Glance
Three designs have become established on CNC gantry milling machines. Each has a specific target application, and the choice depends on floor space, number of tools and the desired change speed.
| Criterion | Linear magazine | Carousel magazine | Pickup magazine |
|---|---|---|---|
| Number of tools | 6–12 | 12–24 | 4–8 (modularly expandable) |
| Change time (chip to chip) | 6–10 s | 3–6 s | 10–15 s |
| Space requirement | Along the machine edge | Compact at the side or above the table | On the machine table |
| Suitable for | Standard trades, joinery | Series production, industry | Beginners, occasionally many tools |
| Investment costs | Low to medium | Medium to high | Low |
Linear magazine (also in-line magazine): the tool holders stand in a row at the edge of the machine table. The spindle moves to the desired position, deposits the old tool and picks up the new one. Advantage: simple mechanics, low maintenance. Disadvantage: takes up space at the side.
Carousel magazine: the tools rotate in a carousel or plate. The spindle only moves to the change position, and the magazine turns the right holder into place. Faster and more compact, but with more mechanics.
Pickup magazine: tools lie in a holder directly on the machine table. The machine moves to the tool, picks it up or puts it down. Very low-cost, but slower, and the magazine area must not be driven over, which costs working area.
SK30 vs. HSK vs. ER: which tool holder suits what?
When choosing the tool holder, three factors matter: repeatability, speed and investment. SK30 is the all-rounder, HSK the high-performance solution, ER the low-cost entry system.
| Property | SK30 (steep taper) | HSK-A/E (hollow shank taper) | ER collet |
|---|---|---|---|
| Standard | DIN 69871 / ISO 7388 | DIN 69893 | DIN 6499 |
| Maximum speed | up to approx. 24,000 rpm | up to 60,000+ rpm | up to 24,000 rpm (spindle-dependent) |
| Repeatability | ≤ 5 µm | ≤ 3 µm | 10–20 µm (manual change) |
| Automatic change | Yes, standard | Yes, premium | No (except with a changing system) |
| Holder cost | Low | High | Very low |
| Typical application | Wood, aluminium, non-ferrous metals | HSC, steel, high speeds | Entry-level CNC, manual operation |
For the vast majority of wood, plastic and aluminium machining, SK30 is the most economical choice. HSK only pays off when speeds above 24,000 rpm are used or high-precision steel machining is involved, typically with HSC machines such as the BZT PFX series. ER remains the standard for entry-level CNC machines without a tool changer. If you want to upgrade later, you can often swap the spindle for an SK30 variant, see Spindles & Motors.
Tool Breakage Monitoring and Tool Length Measurement
An automatic tool changer is only half the battle. For the machine to run truly autonomously, it must check the tool length after every change and detect during operation whether a cutter has broken. There are two solutions for this:
Mechanical tool length probe: A spring-mounted measuring plate on the machine table. The spindle moves the tool up to contact, and the controller stores the Z position. Robust, low-cost, sufficient for most applications. Repeatability approx. 5–10 µm.
Laser tool setter (non-contact): A laser beam at the table edge. The rotating tool interrupts the beam, and the controller records length and diameter. Advantages: faster (measurement in 1–2 seconds instead of 5–10 seconds), no contact, tool breakage monitoring possible during operation. Disadvantage: higher investment (mid four-figure range).
For series production we recommend the combination of ATC plus laser tool setter: the machine detects a tool breakage immediately and can automatically change in a sister tool. However, this requires a correspondingly capable controller, as is integrated in our BZT controllers.
When does an ATC pay off?
The investment in a tool changer is in the mid to high four-figure range, depending on magazine type and spindle size. For this to pay off, the time saved must compensate for the additional cost. A simplified ROI calculation:
The calculation tips in favour of manual changes if:
- Fewer than three tools per part are used.
- The machine only runs a few hours per week (hobby, prototyping).
- Tools would regularly have to be re-measured or changed manually (e.g. rare special tools).
If you are unsure whether an ATC is worthwhile, you can go through a short consultation with us. We work it out pragmatically with your quantities.
BZT Machines With SK30 Tool Changer
BZT offers the SK30 tool changer as standard or as an option on several series. The magazine size and magazine type are matched to the respective part size:
- PFE series: professional entry level for workshops, ATC SK30 with linear magazine (6–10 tools) as an option. Ideal for joinery and occasional aluminium machining.
- PFU series: universal machine with large travel ranges, ATC SK30 with linear or carousel magazine (8–16 tools). Standard solution for furniture making and sign making.
- PFH series: industrial series with Bosch Rexroth linear guides, ATC SK30 as standard, carousel magazine with up to 24 tools plus laser tool setter.
- PFG-S: large-format gantry mill with carousel magazine, optionally also HSK holder for the highest requirements.
The milling spindles typically come from Hiteco, one of the established European spindle manufacturers. Which spindle-magazine combination fits best depends on the material and the typical tool length. You will find an overview of all series with travel ranges and options in the series comparison.
Retrofitting: Is It Possible?
The most common question from existing customers: “Can I retrofit my BZT machine with a tool changer later?” The answer depends on three factors: machine frame, spindle and controller.
Frame: On the large series (PFU, PFH, PFG-S), the mechanical preparation for a linear or carousel magazine is generally possible. On compact machines (PFI, PFK, PF), the footprint is so tight that only a pickup magazine makes sense.
Spindle: An existing ER spindle cannot be converted to SK30 afterwards, because the holder is integrated in the design. Instead, the complete spindle is replaced. This is feasible, but costs mid four-figure sums.
Controller: The controller must support ATC functions (T commands, automatic measuring, tool table). With the BZT controllers this is consistently the case; older third-party controllers may have to be upgraded.
Rule of thumb: a retrofit is worthwhile if the machine still has an expected service life of at least 5 years and the ROI calculation is positive. With very old machines, buying a complete new machine is usually more economical. You can get an honest assessment from us on request.
Frequently Asked Questions
What exactly does SK30 mean?
SK30 stands for “Steilkegel size 30” (steep taper size 30) according to DIN 69871. It is a standardised tool holder available worldwide, with a 7:24 taper, a pull stud for clamping and a typical maximum speed of 24,000 rpm. It is the standard for milling spindles in wood, plastic and aluminium machining.
How fast does an ATC change a tool?
A carousel magazine manages the tool change, including approach and measuring, in 3–6 seconds (chip to chip). A linear magazine takes 6–10 seconds, a pickup magazine 10–15 seconds. Compared with a manual change (60–180 seconds), this is a time saving by a factor of 10 to 30.
Can I retrofit a tool changer?
On medium-sized and large BZT series such as PFU, PFH or PFG-S, a retrofit is generally mechanically possible. Prerequisites: an SK30 spindle or a spindle swap, an ATC-capable controller and sufficient floor space. On compact entry-level series, a pickup magazine is usually the only sensible solution. We are happy to clarify this individually.
SK30 or HSK: which is better?
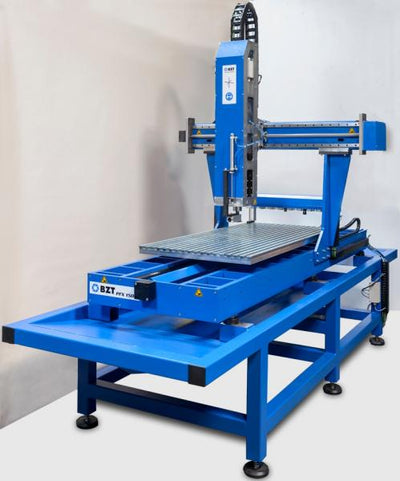
For typical wood, plastic and aluminium machining, SK30 is more economical and sufficiently precise. HSK only pays off when speeds above 24,000 rpm are used, high-precision steel machining is involved or HSC applications are planned. This is typically the case with industrial series such as PFX, not with standard gantry mills.
How many tools fit into a typical magazine?
Pickup magazines usually hold 4–8 tools, linear magazines 6–12, carousel magazines 12–24. For high-volume production there are also chain magazines with 30–60 positions. The choice depends on how many different tools a typical part needs: five to eight are enough for most wood and aluminium parts.
Conclusion: SK30 Is the Standard for Serious CNC Machining
An automatic tool changer with SK30 holder is the most economical step from hobby to professional machining. The holder is robust, available worldwide and well dimensioned for typical wood, plastic and aluminium machining. Anyone who regularly works with more than three tools or produces series recovers the investment in an ATC within a few months.
Which machine and which magazine type fit best depends on part size, number of tools and quantity. A short consultation with us often saves a lot of money: we configure the machine pragmatically for your application. You will find all series with an ATC option in our overview CNC gantry milling machines.


0 comments