

Today’s joinery workshop sits between two worlds: traditional one-off craftsmanship on the one hand, industrial panel machining on the other. A modern CNC gantry mill combines both. It drills fitting patterns reproducibly, routes carcass joints in seconds, cuts door fronts to their contours and makes decorative routed cuts that would cost half a shift by hand. If you spend more than a few hours a week in a joinery workshop marking out, drilling and sawing recurring parts by hand, you usually have a realistic investment case.
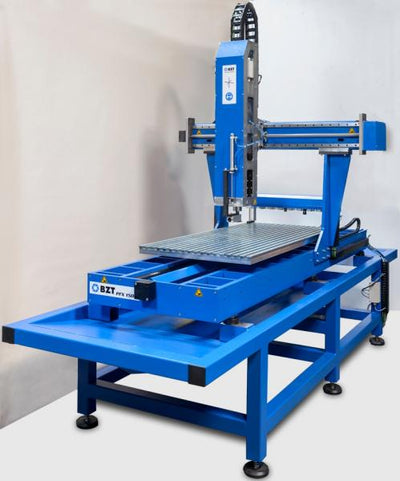
This guide shows in concrete terms at what workshop size a CNC gantry mill pays off, which BZT series suits which workpieces, which spindles and tools are typical, and what to watch for when it comes to installation, dust extraction and software. The travel ranges and recommendations given come from the portfolio of BZT Maschinenbau GmbH, a German manufacturer that has been building CNC gantry mills in Leopoldshöhe since 2006.
When does a CNC gantry mill pay off in a joinery workshop?
A CNC milling machine does not replace a table saw, a panel saw or an edge banding machine. Above all it replaces manual marking out, repeated drilling, contour cutting, slot routing and front machining. The following triggers typically speak in favour of buying one:
- Recurring carcass joints: rows of hinge cup holes, dowel patterns or Lamello slots on several components per job.
- Series fronts: if you make identical or similar drawer fronts, doors or cover panels several times a month.
- Decorative routed cuts: V-grooves, profile engraving, chamfers and contours on visible surfaces that would be too slow or too untidy by hand.
- Fitting holes: reproducible drilling patterns for cup hinges, drawer runners and connectors.
- Contour cutting: curved table tops, seating benches, stair strings or interior fit-outs with organic shapes.
- Lettering and engraving: door signs, furniture markings, interior fit-outs with logos or lettering.
As a rough rule of thumb for ROI: as soon as your workshop regularly has more than 8 to 10 hours a week of manual marking-out, drilling and contour work that a CAD operator could design in advance, the investment in a professional gantry mill from the BZT PFE or PFU range usually pays for itself within 18 to 30 months. For interior fitters doing one-off work this can take longer, and for series furniture manufacturers it is much quicker.
Workpiece Sizes and Travel Ranges: Which BZT Series Is Right?
The key question in the joinery workshop is: how large are my workpieces today, and how large will they be tomorrow? A machine that only takes half sheets blocks you with the next kitchen front. A machine that handles whole board formats needs correspondingly more space. The following overview shows typical workpieces against the BZT series.
| Criterion | BZT PFE | BZT PFU | BZT PFL | BZT PFG-S |
|---|---|---|---|---|
| Travel X | 510–1510 mm | 1010–3020 mm | XL format | 2020–8020 mm |
| Travel Y | 510–1010 mm | 1010–2010 mm | XL format | 1510–3020 mm |
| Travel Z | 160–250 mm | 200–300 mm | XL (for stacked boards) | 300–600 mm |
| Carcass parts (side panel, base) | Up to 1500 x 1000 mm | Up to 3000 x 2000 mm | Full format | Large format / oversize |
| Doors and fronts | Very good for drawers, small doors | Complete kitchen door series | XXL doors, solid wood | Large-format fronts, sliding doors |
| Full chipboard sheet 2500 x 1250 mm | No (too small) | Yes, ideal | Yes, with reserve | Yes, several in parallel |
| Typical application | Joinery workshop with one-off and small-batch work | All-round furniture making, kitchen production | Large-format joinery workshop, interior fit-out | Industrial series, contract work |
An important factor is the Z height, that is, the travel on the vertical axis. Joiners often underestimate it. If you only machine MDF boards 2 cm thick, 110 to 160 mm is enough. If, on the other hand, you want to machine several boards stacked (for example to route drawer sides in one setup) or load solid components such as stair strings, table legs or the stiles of a wooden door, you need 200 to 300 mm. This is exactly where the BZT PFU comes in with its tall gantry.
Understanding Board Sizes: 2500 x 1250 mm and More
Three board formats dominate in Central Europe. Anyone planning a CNC gantry mill for a joinery workshop should know these formats inside out.
- Standard chipboard / MDF: 2500 x 1250 mm. This is the bread-and-butter format of the furniture industry. A machine with less than 2500 mm of travel in X is too small for serious furniture production. This is where the PFU series begins.
- XL format: 2800 x 2070 mm, common for coated chipboard and HPL laminate. If you work with XL boards, you need either a PFU 3020 or a larger series.
- Special sizes: table tops, sliding doors or edge-glued solid wood panels can be 3000 mm and longer. This is where the PFH or PFG-S come into play.
Important: the nominal travel is not the same as the usable clamping surface. Workholding, vacuum zones or stops reduce the usable area by typically 30 to 80 mm per side. So if you want to machine exactly 2500 mm, you should plan for at least 2600 mm of travel.
Workholding and Vacuum Tables
In the joinery workshop, workholding decides machining speed, repeatability and operating comfort. Three systems dominate.
- T-slot plates with strap clamps: classic, robust, inexpensive. Ideal for individual parts and solid wood. Disadvantage: with every new setup the strap clamps have to be repositioned, which takes time.
- Vacuum table (grid vacuum table): mandatory for series production of sheet materials. A vacuum table holds the board down through holes or vacuum cups and allows machining right up to the edge. Advantage: setup in seconds. Disadvantage: it needs a powerful vacuum pump and, if necessary, an MDF spoilboard.
- Hybrid solutions: a combination of a T-slot plate with a vacuum grid placed on top. Offers maximum flexibility.
BZT gantry mills can be configured for both worlds from the factory. Matching workholding, clamps, spoilboards and stops can be found under CNC accessories. For joinery workshops with a high board throughput, a grid vacuum table is almost always more economical than repeated mechanical clamping.
Tools for the Joinery Workshop
Carbide end mills and indexable-insert cutters dominate in furniture making. Anyone who wants to cover all the tasks of a modern joinery workshop typically keeps the following tool range on hand:
- End mills, carbide, 1- and 2-flute: 3, 4, 6, 8 and 12 mm diameter for contour milling, slots and pockets.
- Spiral flute cutters (up-cut and down-cut): up-cut for a clean underside, down-cut for a clean top surface. Compression cutters combine both for coated boards.
- V-groove / engraving cutters: 60°, 90° and 120° for lettering, folding edges and decorative V-grooves in visible fronts.
- Drill bits, carbide: blind-hole drill bits 5 mm and 8 mm for hinge cup holes, dowel drill bits.
- Indexable-insert cutters: for high throughput and long tool life on sheet materials.
- Profile cutters: for door panels, glazing bars and profiled edges.
The tools run in an HF spindle with ER collets (typically ER20 or ER25) or, on larger machines, in ISO30/HSK63F tool holders with an automatic tool changer. For joinery workshops with frequent tool changes, an automatic tool changer (ATC) is an enormous time saver.
Dust Extraction: Mandatory for Woodworking
Wood dust is a health risk and a fire risk. A CNC milling machine that runs for several hours a day produces quantities of chips and dust in the joinery workshop that a normal workshop vacuum cleaner cannot handle. A professional extraction system is therefore not an option in the joinery workshop but a must.
A dust shoe with a brush skirt sits on the spindle and picks up the chips directly at the tool. The shoe must match the spindle and the height of the machine. At BZT, these components are part of the configuration kit system.
CAM Software for Joinery Use
The hardware is only one half of the equation. At least as important is the software you use to turn a design into runnable G-code. The following programs have become established in the joinery workshop:
- VCarve Pro / Aspire (Vectric): very popular in the English-speaking world, good for 2D and 2.5D work, V-grooves and contours. In the mid-price range.
- Estlcam: a German solution, very widespread among hobbyists and small joinery workshops. Beginner-friendly, inexpensive.
- Alphacam / WoodWOP: professional industry solutions for furniture production. Wide range of functions, higher price, steep learning curve.
- RhinoCAM / Fusion 360: universal 3D CAM packages, good for complex contours, organic shapes and 3D carving.
- VCarve / SheetCAM: lean solutions for pure sheet machining.
The BZT controllers work with standard G-code, so practically any CAM software can be used. If you need a post-processor, you get it from us or from the respective software vendor.
Installation in the Workshop: Power, Floor, Space
Before the machine is delivered, the workshop must be prepared. The most important points:
- Power supply: professional gantry mills need three-phase power (400 V). For most BZT machines a CEE 16 A connection is enough. With large spindles and an ATC, a 32 A connection may be needed.
- Compressed air: if you use an automatic tool changer or pneumatic clamping elements, you need an oil-free compressor with at least 6 bar and sufficient delivery volume.
- Floor: a stable concrete slab is mandatory. Wooden floors or light steel structures lead to vibration and oscillation that ruin the surface quality.
- Space requirement: add at least 1 m of operating space per side to the nominal machine dimensions. For a PFU 2515 with a footprint of 3.5 x 2.5 m, you should therefore plan for a site of at least 5.5 x 4.5 m.
- Loading and unloading: lifting full boards of 2500 x 1250 mm as a two-person job is arduous. A lifting aid or a lateral board lift saves shoulders and backs.
- Lighting: especially during setup and tool changes, bright, shadow-free lamps help.
Practical Recommendation by Workshop Size
If you are unsure which configuration suits your own workshop, you should seek advice before investing. The key factors are too individual for a blanket answer, from the job structure and the board formats to the number of operators. You can get free advice via our contact form.
Frequently Asked Questions
Which CNC milling machine for a small joinery workshop?
For a joinery workshop of 1 to 3 people with one-off work and the occasional small batch, the BZT PFE with travel ranges from 1010 x 510 mm to 1510 x 1010 mm is usually ideal. It handles typical furniture parts, drawer fronts and doors, is attractive in price and fits into a workshop without taking much space. If you regularly want to machine full chipboard sheets of 2500 x 1250 mm, you should choose the BZT PFU instead.
Can I machine a whole chipboard sheet?
Yes, provided the machine is dimensioned accordingly. For full standard boards of 2500 x 1250 mm you need a machine with at least 2600 mm of travel in X and 1300 mm in Y. In the BZT portfolio this starts with the PFU 2515. For XL formats of 2800 x 2070 mm or larger doors, the PFL or PFG-S are candidates.
Which software do I need for furniture-making CNC?
For standard applications in the joinery workshop, 2D and 2.5D CAM programs such as VCarve Pro, Estlcam or SheetCAM are sufficient. If you want to digitalise carcass joints, dowel patterns and complete furniture production, you should turn to Alphacam, WoodWOP or similar industry solutions. BZT machines with a standard CNC controller process G-code from practically any CAM software.
How loud is a CNC milling machine in the workshop?
The noise level depends mainly on the spindle, the tool and the dust extraction. The machine itself runs quietly. Typical sound pressure levels in operation are between 75 and 90 dB(A), depending on the tool and material. The extraction system often contributes more to the noise than the milling machine. Hearing protection is mandatory in continuous operation.
Do I need three-phase power for a professional CNC milling machine?
Yes, all professional BZT gantry mills from the PFE series upwards need a 400 V three-phase connection. For most configurations a CEE 16 A connection is enough; larger spindles or automatic tool changers require 32 A. A 230 V connection (single-phase) is only sufficient for pure hobby benchtop mills such as the PFI, which are not designed for serious joinery operation.
Are you wondering which BZT series suits your joinery workshop? Compare all models directly in the series comparison or request individual advice via the contact form. We configure your machine to match the workpieces you actually make.




0 comments