

Aluminium is regarded as a classic in CNC machining, but it is anything but undemanding. While a wood router merely lifts off chips, a CNC gantry milling machine for aluminium has to cope with high cutting forces, heat generation and tight tolerances. Anyone who chooses the wrong machine gets smeared chips, rattling contours, chattering tools and, in the worst case, a broken cutter in the workpiece.
The central question is therefore not: “Can I also mill aluminium on this CNC machine?” but: “Is the machine built so rigid, so powerful and so precise that it machines aluminium durably and with repeatable accuracy?” In this article, we clarify what matters technically, which BZT series are suitable for which use, and which typical mistakes you should avoid.
What a CNC Milling Machine Must Deliver for Aluminium
Aluminium is not a homogeneous material. A soft wrought alloy such as EN AW-5083 behaves differently from a tough AlMgSi material (6082) or a high-strength AlZnMgCu (7075). What they all have in common: aluminium likes to stick to the tool, builds up heat and demands a clean, sharp cut. A CNC gantry mill needs a certain basic specification for this.
Rigidity and Machine Frame
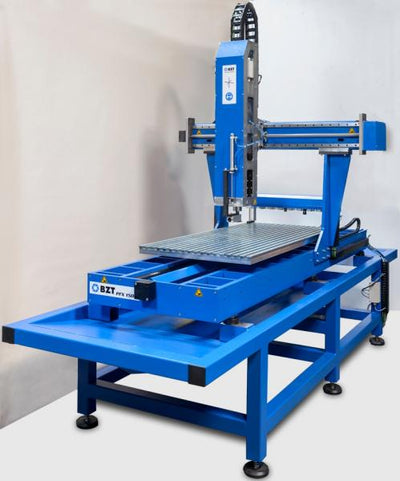
The most important factor is rigidity. If the gantry vibrates under cutting force, chatter marks appear on the workpiece surface and the cutter breaks more often than average. Hobby machines with an aluminium profile frame can only manage this with very small depths of cut. Real aluminium machining requires a bolted or welded steel frame, as in the BZT PFE, PFU and PFH series. The heavy steel and aluminium cast composite constructions dampen vibrations and hold the gantry in position even under load.
Drive: Ball Screw Instead of Toothed Belt
Belt-driven axes are inexpensive and often sufficient for wood. As soon as aluminium comes into play, belt elasticity becomes a problem: it flexes under feed force, which leads to contour errors and uneven chip removal. Ball screws, on the other hand, transmit the rotary motion practically without play and rigidly. All BZT models from the PFE series upwards are fitted as standard with high-quality ball screws on all three axes.
HF Spindle from 1.5 kW
An 800 W spindle from China is not enough for aluminium. Aluminium needs spindle speeds beyond 18,000 rpm together with stable torque. A high-frequency (HF) spindle from 1.5 kW, preferably 2.2 kW, is mandatory. If you mill series parts or work with large tool diameters, choose 3 or 5 kW. Water-cooled spindles run more quietly and last longer than air-cooled ones because they reliably dissipate heat.
Cooling and Lubrication
Aluminium needs lubrication, and that is that. Without minimum quantity lubrication (MQL) or mist cooling, the chip welds to the tool, creating what is known as “built-up edge”. The result: poor surfaces, tool breakage and, in extreme cases, aluminium melting at the cutting edge. An MQL system with ethanol or a special aluminium cutting fluid solves the problem reliably. Spray mist consumes only fractions of a millilitre per minute and leaves an almost dry workpiece surface.
Controller and Feed Rate Control
The CNC controller has to be able to coordinate feed rate and spindle speed exactly. Look-ahead functions, smooth acceleration ramps and a reliable override control are decisive when milling aluminium, because even small feed rate fluctuations can overload the cutter. BZT supplies its machines with the built-in WinPC-NC controller or with an optional Eding CNC; both are very well suited to aluminium CAM programs.
Hobby, Workshop, Series Production: Three Classes for Aluminium
Not everyone who wants to mill aluminium needs a €30,000 industrial machine. But equally, a €2,500 hobby milling machine is no good for daily series parts. The following overview assigns the typical use cases to the appropriate machine classes.
Class 1: Hobby & Model Making
You mill a few aluminium brackets, RC parts or decorative signs per month. Workpiece sizes under 700 x 500 mm, material thicknesses up to 10 mm. A compact gantry mill with a steel frame, ball screw drives and a 1.5 kW spindle is enough here. Important: small depths of cut, high spindle speeds, a steady hand with the CAM parameters.
Class 2: Workshop & Commercial Use
Aluminium is part of your everyday work, but not the only material. You mill front panels, fixtures, prototypes, sign making with aluminium composite panels and occasionally solid material as well. Here you need a machine that handles wood and plastic just as well as aluminium up to 20 mm thick. Larger working area, 2.2 kW spindle, mist cooling as an option.
Class 3: Series Production & Industry
You produce aluminium parts on a recurring basis, if applicable in batch sizes, with tight tolerances and specified surface finishes. What counts here is not only cutting speed but also repeatability, component service life and the option of automation (tool changer, 4th axis, vacuum table). The machine has to be able to mill aluminium for 8 hours at a stretch without accuracy or tool life suffering.
BZT Models for Aluminium Machining
The following table shows which BZT series is built for which aluminium requirement. All figures are guideline values; the exact configuration (spindle power, travel ranges, options) depends on the specific model.
| Criterion | PFK | PFE | PFU | PFU-S | PFH | PFX |
|---|---|---|---|---|---|---|
| Travel X | 300–720 mm | 510–1510 mm | 1010–3020 mm | 1010–3020 mm | 1010–6020 mm | 1010–2020 mm |
| Travel Y | 300–420 mm | 510–1010 mm | 1010–2010 mm | 1010–2010 mm | 1010–3020 mm | 1010–1510 mm |
| Spindle recommendation | 1.5 kW | 2.2 kW | 2.2–3 kW | 3–5 kW | 5 kW+ | HSC spindle |
| Aluminium suitability | Occasional | Regular | Regular, large | Series | Industry | High precision |
| Typical application | Hobby parts, signs | Front panels, fixtures | Large-format panels, model making | Series parts, mould tooling | Industrial parts, steel mix | Mould making, high-precision parts |
| Price level | Entry | Medium | Medium-high | High | Industry | Industry |
Anyone buying in the middle range (PFE or PFU) gets a machine that machines aluminium with confidence and is equally at home in wood and plastic. For pure aluminium workshops or series production, the step up to the PFH class with reinforced Bosch Rexroth linear guides is worthwhile.
Cutting Data and Tool Selection for Aluminium
Even the best machine is useless if the cutting data do not fit. Aluminium forgives mistakes less than wood: too slow a feed rate smears, too fast a depth of cut breaks the tool. The following guideline values apply to a typical wrought aluminium alloy (e.g. AlMg3 / EN AW-5754) and a 6 mm solid carbide end mill with two flutes:
- Spindle speed: 18,000–24,000 rpm
- Feed rate: 1500–3000 mm/min
- Axial depth of cut (ap): 50–100% of the tool diameter
- Radial depth of cut (ae): 25–40% for roughing, 5–10% for finishing
- Chip volume: As large as possible, because small chips stick and large chips carry heat away
For tools, the following applies: sharp grind, polished flute, chip spaces as large as possible. Standard cutters for steel are unsuitable for aluminium because their cutting edge geometry is designed for compressive chips. Choose tools ground specifically for non-ferrous metals:
- Carbide end mills, 2-flute: Standard for aluminium, large flute
- Carbide end mills, 3-flute: Better surface finish, somewhat higher feed rates
- Diamond-coated tools: Long tool life, especially with high-silicon alloys
- Polished flute: Reduces sticking (“Aluminium Polish” or “Bright Finish”)
If you want to source tools and auxiliary materials, you will find a preselected range of end mills, clamping devices and measuring tools in the BZT accessories shop.
Spindle Power: How Many kW Does Aluminium Need?
The spindle question is the most frequently asked question when milling aluminium. The short answer: “As much as possible, but at least 1.5 kW”. The longer answer:
- 1.5 kW HF spindle: enough for aluminium up to approx. 6 mm tool diameter, smaller depths of cut, mainly contour work. Ideal for the PFE entry-level models.
- 2.2 kW HF spindle: the sweet spot for mixed workshop operation. Allows 8 mm cutters at full depth of cut, faster feed rates, better tool life. Standard equipment for the PFE 1300 and larger PFU models.
- 3–5 kW HF spindle: for series production and large tool diameters. No speed drop under full load, very smooth running. Recommended for the PFU-S and PFH.
If you want to go deeper into spindle selection, the article on HF spindle selection provides a detailed overview of frequency inverters, cooling, tool holders (ER, HSK, ISO) and maintenance intervals.
Common Mistakes When Milling Aluminium
Most aluminium problems are not caused by the machine but by the wrong strategy. Here are the most common stumbling blocks, and how to avoid them:
- Feed rate too slow. Too small a feed per tooth means the tool does not cut but rubs. Result: heat, sticky chips, built-up edge. It is better to raise the feed rate than to lower the spindle speed.
- Missing cooling. Dry milling only works with very small depths of cut and short engagement. As soon as you machine aluminium regularly, an MQL system is mandatory, not a recommendation but a prerequisite for clean results.
- Wrong tool grind. Universal cutters for “all materials” are a compromise. For aluminium, you need sharp, polished 2- or 3-flute cutters with a large flute.
- Unsuitable machine. A hobby milling machine with an aluminium profile frame will vibrate when milling solid material. The result: chatter marks, tool breakage, frustration. The investment in a rigid machine saves tool and claim costs in the long run.
- Depth of cut too small. Paradoxically, too small a depth of cut is harmful in aluminium. Small chips cannot carry heat away and stick to the tool. The rule of thumb: ap at least 50% of the tool diameter.
- Missing dust extraction. Aluminium chips are sharp-edged and find their way into every guide. A cyclone separator in combination with an industrial extraction system protects the mechanics and ensures safe working.
Frequently Asked Questions
Which BZT milling machine is suitable for aluminium hobby projects?
For occasional aluminium parts in hobby and model making, a compact BZT PFK or PFE with a 1.5 kW HF spindle is enough. Both models have a steel frame and ball screws on all axes, the basic prerequisite for clean aluminium machining. With small depths of cut and proper mist cooling, brackets, front panels and decorative parts up to approx. 15 mm thick can be milled reliably.
Can I also machine aluminium on a wood router?
To a limited extent. A wood router with an aluminium profile frame and toothed belt drive will vibrate when milling aluminium, become inaccurate and wear tools faster. If your machine, on the other hand, has a steel frame, ball screws and a sufficiently powerful HF spindle, like all BZT models from the PFE upwards, you can easily machine aluminium. Additional mist cooling is recommended in any case.
Do I need mist cooling for aluminium?
For sporadic aluminium parts with small depths of cut, you can also work dry, but the results are rarely optimal. As soon as you regularly machine aluminium or thicker material, minimum quantity lubrication (MQL) is mandatory. It prevents chips from sticking to the tool, extends tool life many times over and ensures significantly better surface finishes. MQL systems consume only millilitres per hour and leave workpieces practically dry.
How fast can I mill aluminium on a CNC gantry milling machine?
With a 6 mm solid carbide cutter on a BZT PFE or PFU, feed rates of 1500–3000 mm/min at 20,000 rpm are realistic and gentle on the tool. On larger machines such as the PFH with a 5 kW spindle and 10 mm tools, significantly higher chip volumes can be achieved. However, the speed depends heavily on workpiece geometry, clamping and tool quality; there is no blanket “aluminium speed”.
What spindle power is optimal for aluminium?
The lower limit is a 1.5 kW HF spindle for occasional aluminium milling. Optimal for mixed workshop operation is 2.2 kW; this power allows 8 mm cutters at full depth of cut and fast feed rates. If you mill aluminium daily or work with large tools, choose 3 to 5 kW. Water-cooled HF spindles are preferable to air-cooled models because they reliably dissipate heat and last longer.
Not sure which BZT series suits your aluminium application? Send us your workpiece specification, planned batch size and desired travel ranges, and we will recommend the suitable configuration. You can request a consultation directly or view the series comparison table.


0 comments