

Milling is ideal for precision machining, but with thick steel plate even the sturdiest gantry mill reaches its limits. This is where CNC plasma cutting comes into play: with a plasma jet hotter than 20,000 °C, you can cut even 30 mm thick steel plate in seconds.
In this guide you will learn how CNC plasma cutting works, what advantages and disadvantages it has compared with milling, and which process suits which application.
What is plasma cutting?
Plasma is the so-called “fourth state of matter”: an ionised, electrically conductive gas. In plasma cutting, a gas jet (usually compressed air, nitrogen or argon) is heated to extreme temperatures by an electric arc: typically 10,000 to 25,000 °C.
The Cutting Process in Detail
The plasma cutting process takes place in several phases:
- Ignition: A pilot arc is ignited between the electrode and the nozzle
- Plasma formation: The gas flowing through is ionised and forms the plasma jet
- Main arc: The plasma jet transfers the arc to the workpiece
- Cutting: The material melts locally, and the gas jet blows the molten metal out of the kerf
- Feed: The CNC controller guides the torch along the programmed contour
The result: a narrow kerf, typically 1–3 mm wide, depending on material thickness and current.
Difference From Other Thermal Cutting Processes
| Process | Temperature | Materials | Max. thickness |
|---|---|---|---|
| Plasma | 10,000–25,000 °C | All conductive metals | 50+ mm |
| Oxy-fuel (flame cutting) | approx. 3500 °C | Unalloyed steel only | 300+ mm |
| Laser | Extremely high at a single point | Almost all materials | approx. 25 mm |
Advantages of CNC Plasma Cutting
Cutting Thick Materials Economically
The biggest advantage of plasma: you can cut steel plate up to 30 mm and more without any problem. At such material thicknesses, milling would be uneconomical or impossible, whereas a plasma torch does it in a single pass.
High Cutting Speed
For simple contours, plasma works considerably faster than milling. Typical cutting speeds:
- 3 mm steel: up to 5000 mm/min
- 10 mm steel: up to 2000 mm/min
- 25 mm steel: up to 800 mm/min
For comparison: a milling machine would need several passes at 200–500 mm/min each for 10 mm steel.
Machining Different Metals
Plasma cuts all electrically conductive materials:
- Mild steel and stainless steel
- Aluminium and aluminium alloys
- Copper and brass
- Cast iron
Low Operating Costs
The consumables (electrode, nozzle, swirl ring) cost about €5–20 per set. Depending on use, a set lasts 1–4 hours. Compared with milling tools for machining steel, this is very economical.
Limits and Disadvantages of Plasma
Lower Accuracy
Plasma cutting typically achieves a dimensional accuracy of ±0.3 to ±0.5 mm. For precision parts, fits or fine details, this is often not sufficient. This is where the milling machine has to rework the part.
Cut Edge Quality
Plasma-cut edges show some particular characteristics:
- Heat-affected zone: The material hardens slightly at the cut edge
- Dross: Dross can adhere to the underside (burr)
- Squareness: The cut edge is slightly angled (1–3°)
- Roughness: Rougher than milled surfaces
For visible edges or fits, rework is often necessary, by grinding or milling.
2D Machining Only
Plasma can only cut vertically through material. Complex 3D shapes, pockets, engraving or threads are not possible. For these you need a CNC milling machine.
Conductive Materials Only
Plastic, wood, composites: plasma cannot machine any of these. The arc needs an electrically conductive workpiece.
CNC Plasma vs. CNC Milling Machine: The Big Comparison
| Criterion | CNC plasma | CNC milling machine |
|---|---|---|
| Steel thickness | Up to 50+ mm without problems | Limited (depends on machine rigidity) |
| Accuracy | ±0.3–0.5 mm | ±0.01–0.1 mm |
| Surface quality | Rough, rework often needed | Finished in one operation |
| Material range | Conductive metals only | Wood, plastic, aluminium, steel, composites |
| Types of machining | Cutting only (2D) | Milling, drilling, engraving, 2D/2.5D/3D |
| Speed on steel | Very high | Lower, several passes |
| Tooling costs | Low (€5–20 per set) | Higher for steel machining |
| Rework | Often required | Usually not necessary |
| Heat input | High (hardening possible) | Low |
When plasma, when milling?
Choose plasma if:
- You want to cut thick steel plate (from 5–6 mm)
- Simple contours without high precision requirements are needed
- Large quantities of sheet metal parts are produced
- Rework is planned anyway
Choose a milling machine if:
- Precision in the hundredths range is required
- 3D machining, pockets, holes or engraving are needed
- Different materials are machined (wood, plastic, aluminium)
- Finished surfaces without rework are desired
Typical Applications for CNC Plasma
Steel and Metal Construction
Cutting plates to size, making cut-outs for pipe penetrations, producing base plates: in steel construction, plasma is indispensable. Typical parts: brackets, connection plates, column bases.
Mechanical Engineering
Base plates, blanks for housings, flanges: plasma cuts the blank, and the milling machine takes over the fine machining of the functional surfaces.
Vehicle Construction and Repair
Frame parts, repair plates, brackets: vehicle construction often requires custom sheet metal parts, which are produced quickly and economically with plasma.
Art and Crafts
Metal sculptures, fire bowls, garden decoration, company signs made from steel: plasma also enables artistic applications with thicker material.
Technical Requirements for a CNC Plasma System
Machine Design
A plasma machine differs fundamentally from a milling machine:
- Torch mount instead of spindle: The plasma torch replaces the milling spindle
- Automatic torch height control (THC): The distance between torch and plate must be kept constant, because plates warp as they heat up
- Cutting table: Water table or downdraft table with slats to catch sparks
- Splash guard: Sparks and molten metal fly, so the machine needs suitable protection
- Dust extraction: Smoke and fumes must be extracted (occupational safety)
Controller
The CNC controller must be designed specifically for plasma:
- THC integration: Automatic height adjustment via arc voltage
- Plasma interface: Communication with the plasma power source (on/off, current)
- Adapted acceleration: Gentler starts for clean corners
- Piercing routines: Special piercing cycles for different material thicknesses
Plasma Power Source
The plasma power source determines the cutting capacity:
- 40–60 A: For thin sheet up to 10 mm
- 80–100 A: Universal for 3–20 mm
- 120–200 A: For thick plate of 20–40 mm
- 300+ A: Industrial systems for extreme applications
BZT Plasma Solutions
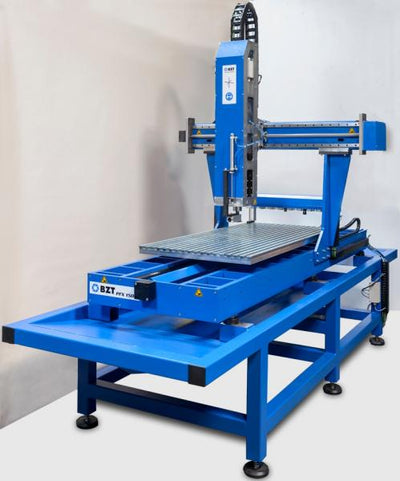
As a manufacturer of CNC gantry milling machines, we also offer a CNC machine designed specifically for plasma cutting with the PFU-G Plasma.
Features of the PFU-G Plasma:
- Robust steel construction for tough plasma operation
- Integrated plasma control with THC
- Water table or downdraft table, as required
- Various working sizes available
- On request: combination with a milling spindle for both processes
BZT tip: Many of our customers use a combined solution: plasma for cutting to size, milling for fine machining. This way you get the most out of both processes.
FAQ: Frequently Asked Questions About Plasma Cutting
Can I convert my existing CNC milling machine to plasma?
In principle this is possible, but not recommended. Milling machines are not designed for the thermal load, flying sparks and smoke generated during plasma cutting. A dedicated plasma machine or a specially designed combination machine is the better choice.
How loud is plasma cutting?
Plasma cutting is louder than milling, typically 90–100 dB. Hearing protection is mandatory. With a water table, the noise level is considerably lower (approx. 75–85 dB).
Which gases are used for plasma?
Most commonly, compressed air is used, which is low-cost and sufficient for most applications. For better cut quality on stainless steel, nitrogen or a nitrogen-hydrogen mixture is often used. For aluminium, argon-hydrogen improves the results.
Conclusion: Plasma and Milling Complement Each Other Well
Plasma cutting is not a substitute for CNC milling, but a very good complement. The strengths of the two processes lie in different areas:
- Plasma: Rough cutting, thick material, high speed, low cost per cut
- Milling machine: Precision, 3D machining, material variety, finished surfaces
Many successful businesses therefore use both technologies: plasma cuts the blanks to size, and the CNC milling machine takes over the precise final machining. This way you combine speed with accuracy.
Related Guides
Would you like to combine plasma and milling? Our technical team will be happy to advise you on the solution that suits your application. Contact us via the contact form or by telephone.




0 comments