

| Cutter Ø | Spindle speed | Feed per tooth | Depth of cut |
|---|---|---|---|
| 3 mm | 20,000–24,000 rpm | 0.05–0.10 mm | up to 1× D = 3 mm |
| 6 mm | 18,000–22,000 rpm | 0.08–0.15 mm | up to 1× D = 6 mm |
| 8 mm | 15,000–18,000 rpm | 0.10–0.20 mm | up to 1× D = 8 mm |
| 12 mm | 10,000–14,000 rpm | 0.15–0.25 mm | up to 0.5× D = 6 mm |
Aluminium is the king of materials in modern mechanical engineering. It is light, strong, corrosion-resistant and, with the right technique, excellent to machine. But this is exactly where the trap lies: Aluminium does not forgive mistakes in cutting data, tool selection or cooling.
This comprehensive practical guide tells you everything you need to know about milling aluminium successfully on a CNC gantry milling machine, from choosing the alloy to surface finish.
Why mill aluminium?
Aluminium is one of the most frequently milled materials, and for good reason:
- Low weight: About one third of the density of steel
- Good strength: Especially high-strength alloys such as AlMgSi or AlZnMg
- Corrosion-resistant: The natural oxide layer provides protection
- Good machinability: Lower tool wear than with steel
- Versatile: From front panels and prototypes to machine components
The Biggest Challenge: Built-Up Edge
The main problem when milling aluminium (especially soft alloys) is called built-up edge. Frictional heat softens the material and it sticks to the cutting edge of the cutter.
What happens with built-up edge?
- The cutter generates heat through friction
- Aluminium becomes soft and plastic
- Material welds itself to the cutting edge
- The cutter stops cutting and instead pushes and rubs
- Even more heat is generated, a vicious circle
- The cutter breaks or the workpiece is ruined
How to Avoid Built-Up Edge
1. Choose the right alloy
Not every aluminium alloy can be milled equally well:
| Alloy | Machinability | Typical application |
|---|---|---|
| AlMg3 (5754) | Very good | Universal, signs, housings |
| AlMg4,5Mn (5083) | Very good | Shipbuilding, pressure vessels |
| AlMgSi (6060, 6082) | Good | Profiles, structural applications |
| AlZnMg (7075) | Good | High-strength parts, aerospace |
| Al99,5 | Poor (gummy) | Avoid for milling |
These values come from our cutting data calculator and are deliberately conservative: they are safe starting values for gantry mills. With a very rigid machine, minimum quantity lubrication (MQL) and a small radial depth of cut, higher spindle speeds are possible in HSC machining; approach them step by step.
Tip: Ask your material supplier specifically for alloys suitable for milling.
2. Cooling and lubrication
Without lubrication, almost nothing works when milling aluminium. Minimum quantity lubrication (MQL) is the standard:
- A fine oil mist directly at the cutting edge
- Cools and lubricates at the same time
- Prevents the material from sticking
- Considerably improves the surface finish
For heavy machining, emulsion coolant can also make sense, but it requires suitable machine equipment.
3. The right tools
Aluminium places special demands on tools:
- Single-flute cutters (single-flute end mills): Large chip space, fast chip evacuation
- Polished flute: Material slides off better and sticks less
- Sharp cutting edges: Less friction, less heat
- Coating: DLC (diamond-like carbon) or uncoated. Do not use TiN.
Cutting Data for Aluminium
Aluminium likes speed, both in spindle speed and in feed rate.
Basic Rule: Cut Fast, Do Not Rub
If the cutter travels through the material too slowly, there is more friction than cutting. This leads to heat and built-up edge.
The values below are guide values. To check them for your specific cutter and machine, use the cutting data calculator.
Guide Values for Aluminium
| Cutter diameter | Spindle speed | Feed per tooth | Depth of cut |
|---|---|---|---|
| 3 mm | 15,900–24,000 rpm | 0.035 mm | up to 1x D = 3 mm |
| 6 mm | 8000–18,600 rpm | 0.050 mm | up to 1x D = 6 mm |
| 8 mm | 6000–13,900 rpm | 0.058 mm | up to 1x D = 8 mm |
| 12 mm | 4000–9300 rpm | 0.071 mm | up to 0.5x D = 6 mm |
Note: These values are starting points. Optimise step by step based on chip formation, noise and surface finish.
Climb Milling vs. Conventional Milling
Mill aluminium using climb milling (the cutting edge rotates in the direction of feed). Advantages:
- Better surface finish
- Less burr formation
- Less vibration
- Longer tool life
Plunging (Ramping Instead of Drilling)
Never plunge straight down into the material. Aluminium is tough: with a drilling motion, enormous heat is generated and the cutter can jam.
Instead:
- Ramp: Enter at an angle (2–5°)
- Helix: Plunge in a spiral
- Pre-drilling: Drill a starting hole, then mill
Which machine for aluminium?
Not every gantry mill is suitable for aluminium. What matters:
- Rigidity: Aluminium requires higher cutting forces than wood or plastic
- Spindle power: At least 2–3 kW for efficient machining
- Cooling option: An MQL connection should be available
BZT Recommendations by Application
For plates, front panels, signs:
- PFU-S: Robust steel construction, ball screws. The all-rounder for aluminium up to 10 mm depth per pass.
- PFE: Low-cost entry point for engraving, thin sheet and light aluminium work.
For heavy machining (heavy stock removal):
- PFH: Heavy: heavy steel construction, optionally with servo motors and HF spindles up to 15 kW. Here you can really remove material.
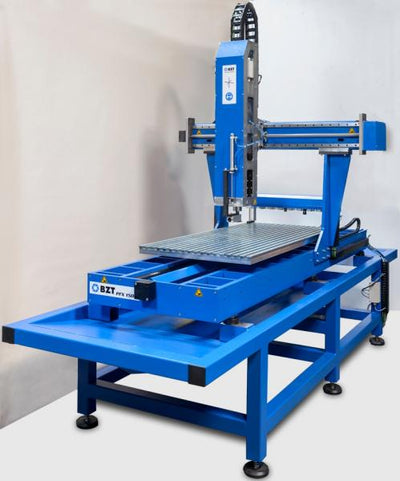
- PFX: HSC machine for high-speed cutting: the highest precision in 3D machining.
For profile machining:
- PFS: Open frame construction, especially for long aluminium profiles (window manufacturing, exhibition stand construction). End-face and surface machining possible.
Surface Finish on Aluminium
With the right technique you can achieve excellent surfaces on aluminium:
What affects the surface?
- Tool condition: Only sharp tools deliver good surfaces
- Feed: A slower finishing feed gives a finer surface
- Depth of cut: Small finishing allowances (0.2–0.5 mm)
- Cooling: MQL clearly improves the surface
- Machine rigidity: No vibration means no chatter marks
Achievable Roughness Values
| Machining | Roughness Ra | Appearance |
|---|---|---|
| Roughing | 6.3–12.5 µm | Clearly visible tool marks |
| Finishing | 1.6–3.2 µm | Fine tool marks |
| Fine finishing | 0.4–0.8 µm | Almost mirror-like |
Typical Applications
Front Panels and Housings
A classic: engraved front panels for measuring tools, control panels and hi-fi equipment. Typically anodised aluminium with engraved-through lettering.
Determine the plate weight in advance (relevant for clamping and shipping): material weight calculator.
Prototypes and One-Off Parts
Fast production of functional prototypes, brackets and adapter plates. Aluminium is ideal for prototypes: light, stable and quick to machine.
Machine Components
Base plates, angle brackets, consoles, motor mounts. Anywhere lightweight construction and corrosion resistance matter.
Model Making
Moulds for deep drawing, casting patterns, lamination moulds. Aluminium polishes well and withstands thermal stress.
Practical Tips for Machining Aluminium
Chip Control
Aluminium chips are long and like to wrap around the cutter. Pay attention to:
- Sufficient dust extraction
- Single-flute cutters (better chip evacuation)
- Regular checks during machining
Workholding
Aluminium is soft, so clamping devices quickly leave pressure marks. Use:
- A vacuum table for thin plates
- Soft jaws in the vice
- Sufficient support surface
Post-Processing
Aluminium is easy to post-process:
- Deburring: Chamfer mill or manually
- Polishing: Polishing paste for a mirror finish
- Anodising: Anodic oxidation for protection and appearance
- Blasting: Matting for an industrial look
Advanced Techniques
HSC Machining (High-Speed Cutting)
HSC uses higher spindle speeds and feed rates, but with a smaller depth of cut. Advantages:
- Better heat removal via the chips
- Reduced thermal load on the workpiece
- Excellent surface quality
- Higher productivity in finishing operations
Pocket Milling With Adaptive Toolpaths
Modern CAM software offers adaptive toolpaths (e.g. Fusion 360, Mastercam). These keep the tool load constant and allow:
- Greater depths of cut (up to 2x diameter)
- Higher feed rates
- More even tool wear
- Less tool breakage
How much the cutter is actually engaged in the corner depends on the path radius: check it in the path radius calculator.
FAQ: Frequently Asked Questions About Aluminium Milling
Can I mill aluminium without cooling?
Only to a very limited extent. For thin engravings or minimal machining, compressed air will do if necessary. For real milling work, MQL is strongly recommended, otherwise you risk tool breakage and poor surfaces.
Which cutter for aluminium, single-flute or multi-flute?
For most applications: single-flute cutters (single-flute end mills). They have more room for chip evacuation and are less prone to clogging. Use multi-flute cutters only on very rigid machines with good cooling.
How do I know whether the cutting data is right?
Watch the chips: good chips are short and comma-shaped with slight discolouration (silver to gold). Bad chips are long strands or blue chips (too hot). Listen to the sound: a steady sawing sound is good, squealing is bad.
Can my wood CNC machine also mill aluminium?
To a degree. Many machines designed for wood can machine light aluminium (engraving, thin plates). For serious aluminium machining, however, you need a more rigid construction and matching spindle power.
Which tolerances are achievable?
With a rigid BZT machine and careful working methods, tolerances of ±0.05 mm are easily achievable. Under favourable conditions (temperature-controlled workshop, precision tools), ±0.02 mm is also possible.
Conclusion: Milling Aluminium Is No Problem With the Right Setup
Milling aluminium is not rocket science when the setup is right. With a stable BZT machine (preferably a steel frame), minimum quantity lubrication, the right tools and adapted cutting data, you will achieve mirror-smooth surfaces and fits in the H7 range.
The short formula for successful aluminium milling:
- Choose an alloy suitable for milling (AlMg3, AlMgSi)
- Use MQL cooling
- Use single-flute, polished cutters
- Cut fast (high spindle speed, high feed rate)
- Use climb milling
- Never plunge straight down
Are you planning aluminium machining on your CNC machine? Our technical team will be happy to advise you on the machine configuration and accessories that suit your application. Contact us.
Recommended Products for Aluminium Machining
- CNC gantry milling machines: machines with sufficient rigidity for aluminium
- HF spindles: high-frequency spindles for high spindle speeds when machining aluminium
- Minimum quantity lubrication: indispensable for machining aluminium
- Solid carbide cutters for aluminium: single-flute cutters and polished two-flute cutters




0 comments